Industries › Recycling
Recycling
Heavy-Duty Conveyor Infrastructure for Sorting, Crushing, and Baling.
Probe supplies enterprise-grade Probe's belting solutions designed to survive the most punishing recycling environments — ensuring your facility maintains continuous, high-volume throughput across waste separation, sorting, crushing, and baling operations in the UAE and GCC.
Engineered for Extreme Belting Challenges
Standard conveyor belts quickly fail under the unpredictable stress of raw waste. We supply purpose-made Probe's belts proven successful by OEMs and end-users globally, specifically engineered to overcome the sector's toughest challenges.
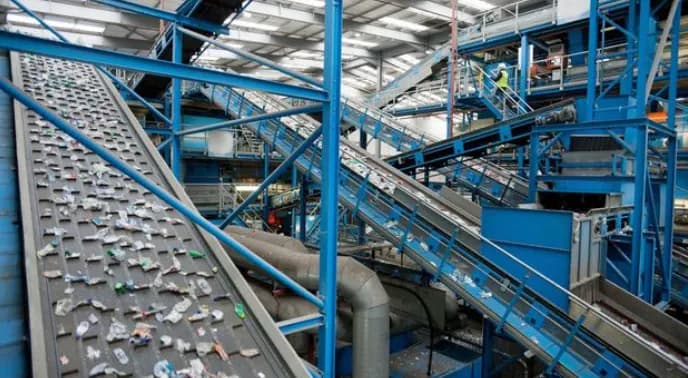
Heavy-Duty Infrastructure for Sorting, Crushing, and Baling
In the rapidly expanding waste management and sustainability sectors of the UAE, converting waste material into new products has become a critical industrial focus. The profitability of a modern recycling plant relies on precision — the better materials are separated, the more valuable they become as raw materials. The mechanical operations required to achieve this place extreme demands on your conveyor infrastructure.
Sector Challenges We Solve
Abrasive & Sharp Materials
Engineered to resist slicing, gouging, and tearing from sharp plastics, shattered glass, and jagged metals. Standard belts quickly fail under these unpredictable stresses.
Heavy Structural Loads
Built with high-modulus tension members to prevent elongation and tracking failures under massive volumes of compacted waste moving through your facility.
Advanced Sorting Compatibility
Specifically manufactured with specialized surface finishes to ensure flawless operation with advanced optical scanners, sorting sensors, and facility cameras for precision material separation.
Key Performance Features
Whether your facility processes commercial plastics or heavy industrial scrap, our belting portfolio delivers uncompromising resilience to extend your operational lifespan.
Abrasion & Tear Resistance
Engineered to resist slicing, gouging, and tearing from sharp plastics, shattered glass, and jagged metals that would rapidly destroy standard conveyor belting.
High Load Capacity
Built with high-modulus tension members to prevent elongation and tracking failures under massive volumes of compacted waste throughout your sorting and baling operations.
Sorting System Compatibility
Specialized surface finishes ensure flawless operation with advanced optical scanners, sorting sensors, and facility cameras for precision material separation and grading.
Wear-Resistant Top Covers
Drastically reduces belt degradation from abrasive materials, lowering your maintenance downtime and total cost of ownership across continuous high-volume recycling operations.
Chemical Resistance
Highly resilient against aggressive industrial chemicals and corrosive liquids often released during crushing and separation processes within the recycling facility.
Oil & Fat Resistance
Specially formulated covers that prevent belt swelling, delamination, and slipping when exposed to industrial oils or organic fats from processed waste streams.
Ready to Solve Your Toughest Belting Challenges?
Our UAE-based engineers evaluate your waste stream characteristics, throughput volumes, and chemical exposure to specify the most resilient belt construction for your facility.