Industries › Airport Baggage Handling
Airport Baggage Handling
Precision Logistics for High-Volume Aviation Infrastructure.
Probe supplies enterprise-grade Probe's conveyor belts designed specifically to ensure the highly effective transfer and precision sorting of baggage items across the UAE and GCC — compliant with ISO 340 flame-retardant standards.
Baggage Handling System Applications
Our belting infrastructure integrates seamlessly into any airport layout, keeping passenger luggage moving safely and rapidly through every system phase.
Engineered for Mission-Critical Aviation Logistics
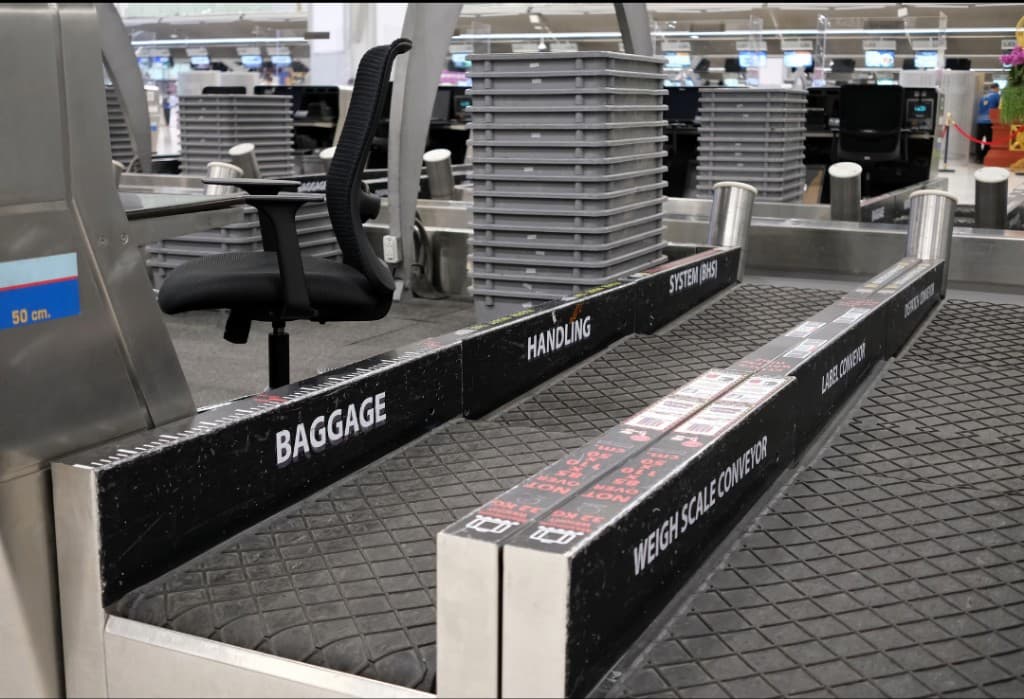
In high-traffic aviation hubs across the UAE and GCC, thousands of suitcases must be transported from check-in counters to aircraft cargo holds — and back — every single hour. Our Probe's conveyor belts are designed specifically to ensure highly effective transfer and precision sorting of baggage items, supporting the complex horizontal, inclined, and curved conveying architectures required by modern international airports.
Core Processing Operations
Check-in Belts
Smooth, highly reliable initial intake systems at passenger counters.
X-Ray Belts
Dimensionally stable, low-interference belts for precise security scanning.
Curve Belts
Seamless directional changes designed to prevent baggage jamming.
Luggage Collection
High-durability surfaces for continuous, heavy-duty passenger retrieval carousels.
Steep & Shallow Inclines
High-grip profiles engineered to prevent slippage during critical elevation changes.
Merger & Diverter Belts
Flawless automated routing designed for high-speed sortation matrices.
Horizontal Conveyor Belts
Long-span, low-stretch transport lines spanning massive terminal infrastructures.
Swing Arm Sorters
Highly responsive belts for rapid, automated lane diversion.
Key Performance Features
Our aviation logistics belts are engineered to meet the strictest international safety and performance standards, ensuring your terminal operates without interruption.
ISO-340 Flame Retardant
Safety in aviation is non-negotiable. Probe produces conveyor belts featuring advanced flame-retardant top cover coatings strictly compliant with the ISO 340 standard.
Low Noise Fabrics
In busy airport environments with multiple conveyor lines running at high speeds, our specialized fabric composition heavily reduces sliding friction, ensuring consistently quiet operation.
Proven Global Reliability
A strong collaboration with international OEMs makes Probe the preferred partner for complex logistics projects across Asia, bringing world-class reliability to the Middle Eastern aviation market.
Unmatched Product Portfolio
With one of the widest ranges of logistics belts available, we supply the exact product for all common terminal applications. Continuous R&D ensures our belts improve mechanical performance and reduce environmental impact.
Ready to Upgrade Your Airport Baggage Infrastructure?
Ensure your terminal's baggage handling systems operate with absolute precision and uncompromising safety. Our UAE-based engineers evaluate load characteristics, speeds, and system integration requirements.